Seven complete component packages, and the operation-by-operation tooling behind each one. Every operation below links to the product that runs it, so you can read this either way round: start from your component, or start from the tool.
The block is the longest tooling list in the engine and the least forgiving. Liner bore, cam and crank bore, deck face, oil galleries, every one of them feeds the next, so a tooled-up block is a single process, not a shopping list of tools.
CYLINDER BLOCK TOOLING · TBD
Operations we tool
Liner bore rough to finish boring, then semi-finish to honing
Cam & crank bore line boring and reaming
Deck face milling and side / mounting face milling
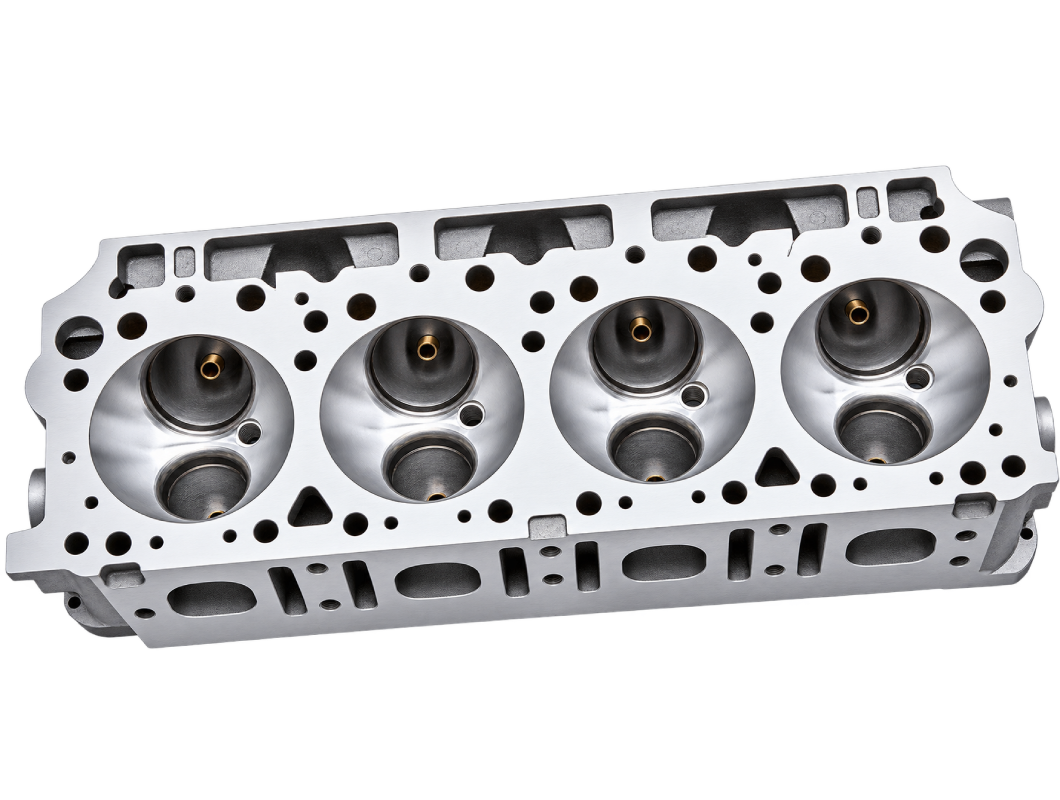
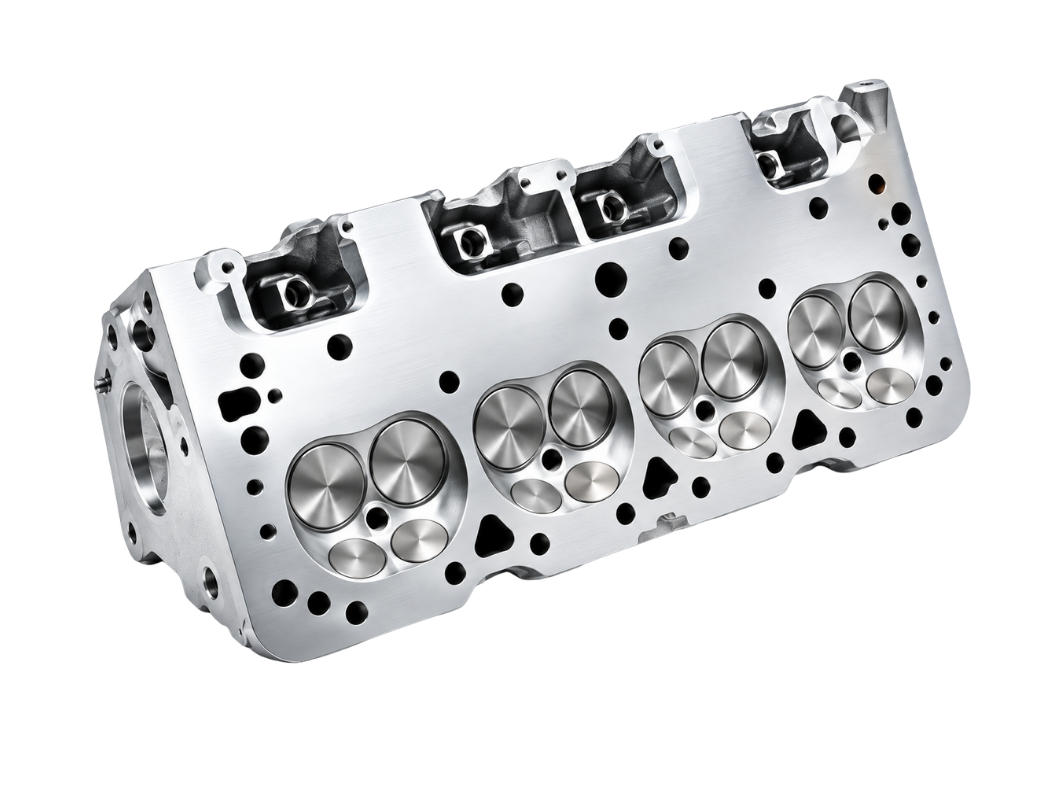
Everything on a head comes back to one relationship: seat concentric to guide. Get it and the valve seals; miss it by a few microns and no amount of downstream accuracy rescues the part. This is the package built around our patented VSVG tooling.
CYLINDER HEAD TOOLING · TBD
Operations we tool
Parent bore roughing and finish parent bore
Valve seat & valve guide boring and reaming
Cam bore boring
Mounting face finish milling and web milling
Drilling, tapping and doweling
Core plug boring
2µmRunout achieved on VSVG tooling
1µmInlet straightness against a 10 µm drawing call
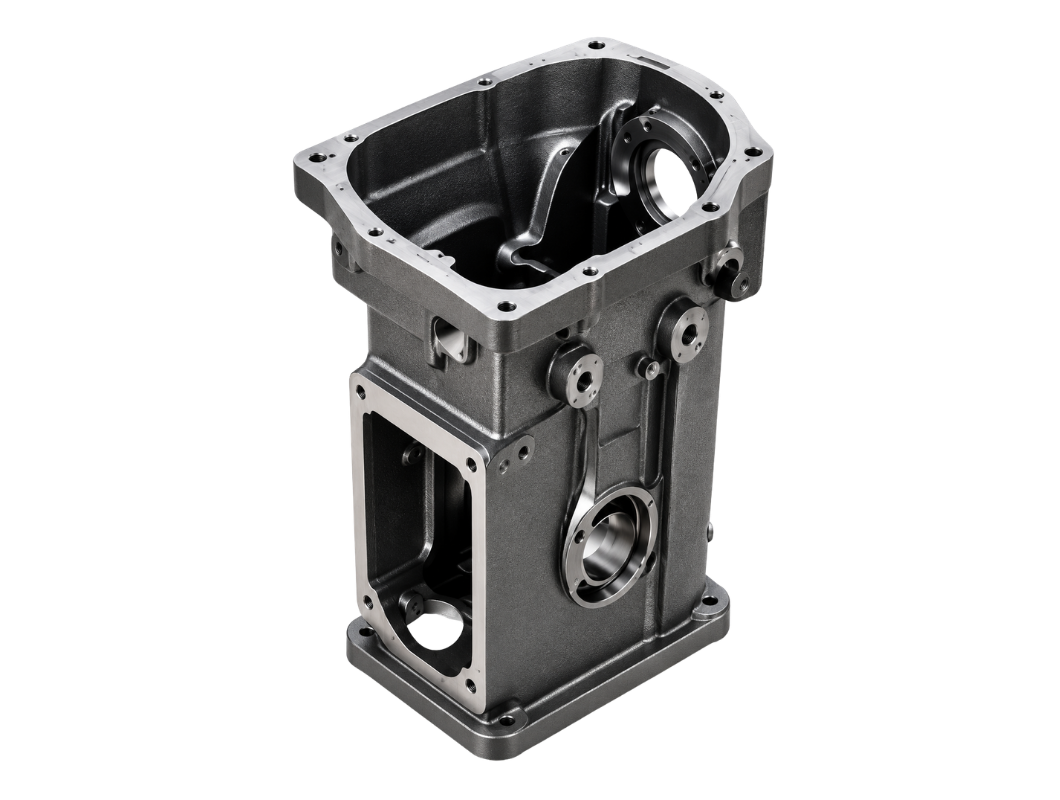
A transmission case is a box of bearing bores that all have to agree with each other. The mounting faces set the datums, the bores carry the gear train, and the whole thing is decided by how few setups you can hold it in.
TRANSMISSION CASE TOOLING · TBD
Operations we tool
Milling of all mounting surfaces
Boring, drilling, tapping & reaming
Bearing bore rough to finish
ID grooving
Doweling and location bore machining
Applies to case transmission, shifter housing and PTO case housing
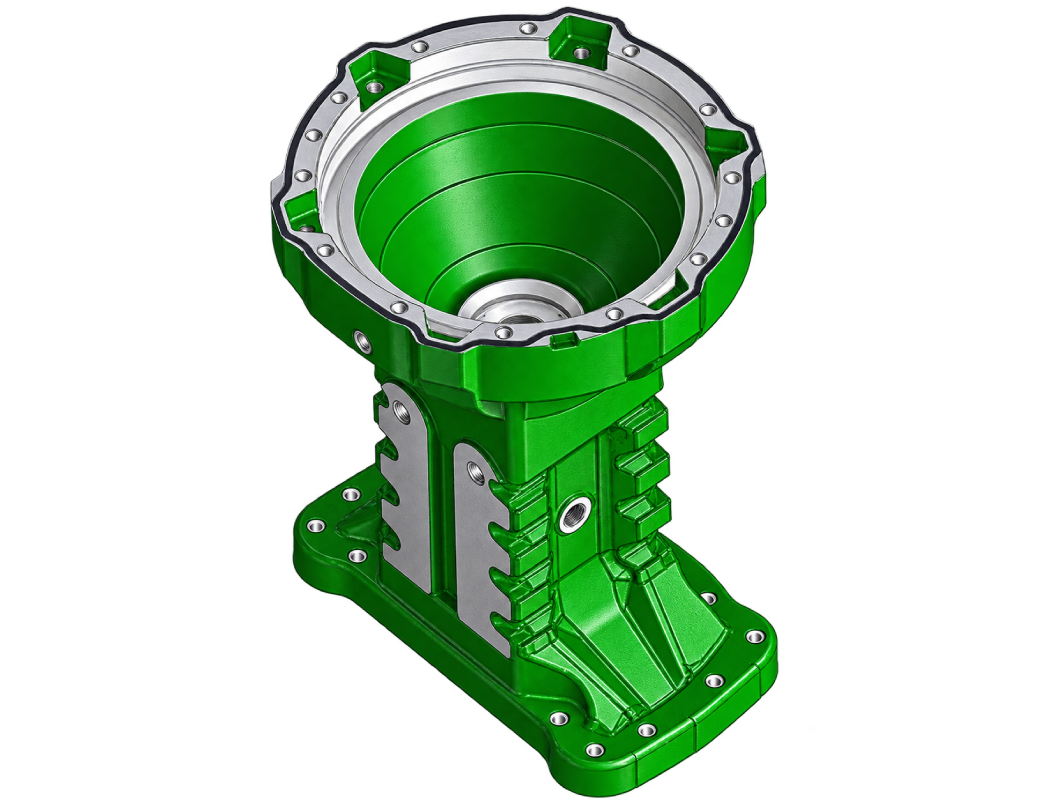
Tractor housings are where overhang becomes the whole problem. The bore is deep, the face is far from the spindle nose, and conventional bars start talking back well before you reach the parameters the cycle time was quoted at.
CENTRE / CLUTCH HOUSING · TBD
Operations we tool
Face milling of all mounting faces
Anti-vibration long boring
Drilling, tapping & doweling
Coaxial bore alignment across the housing
Boring operations rough to finish
Covers centre housing, clutch housing, LB housing and hydraulic lift housing
24×Samurai damping vs conventional AVT
4L/D beyond which conventional bars lose stability
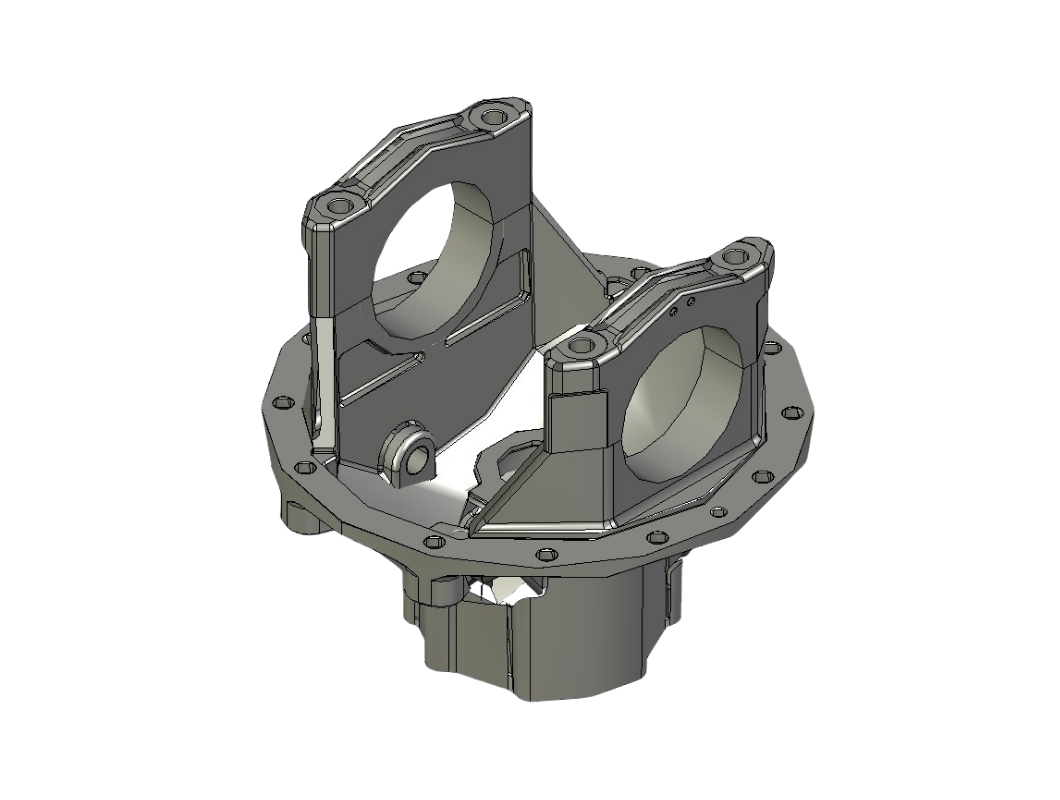
Pinion face, pinion bores inside and out, the differential bore and its thread, four features that have to be true to one axis. Tool it as a set and the axis is established once; tool it piecemeal and you inherit every setup error in the process.
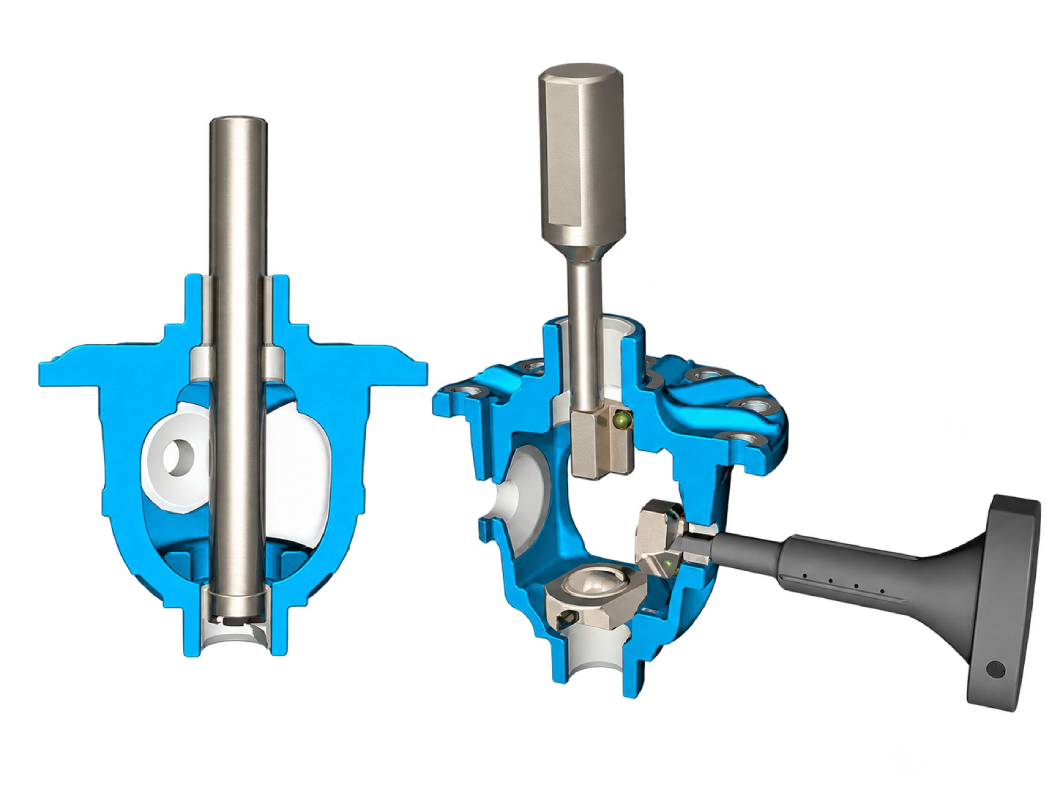
The internal spherical seating is the feature that decides this component, and it is machined blind, through a window, with the tool reaching well past comfortable overhang. Everything else on the case is straightforward by comparison.
DIFFERENTIAL CASE · TBD
Operations we tool
Internal spherical seating
Pinion shaft hole drilling & boring
Face milling of all mounting surfaces
Boring, drilling, tapping & reaming
ID grooving
Differential housing bore and axle tube boring on the banjo drive
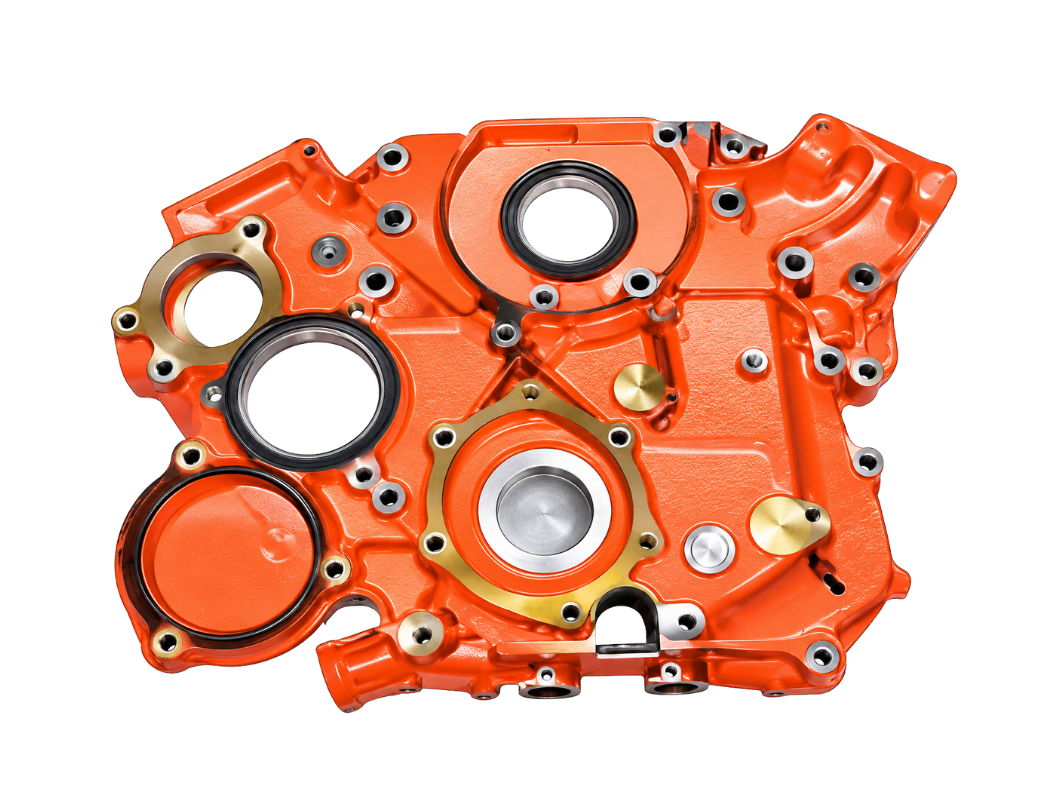
Timing gear case and covers look simple until you count the operations: a large sealing face that has to be flat, a set of bores that have to be round and concentric, and a bolt pattern that has to land on both. Volume makes the cost per edge matter here more than anywhere.
GEAR CASE / COVER · TBD
Operations we tool
Timing gear case face milling
Boring operations, rough to finish
Drilling, tapping & doweling
Oil seal bore finishing
Milling of mating and sealing faces
Covers timing gear case, gear cover and flywheel housing